
Last updated: August 2026 · Reviewed by the Vivid Metrawatt induction engineering team, Mumbai
Table of Contents
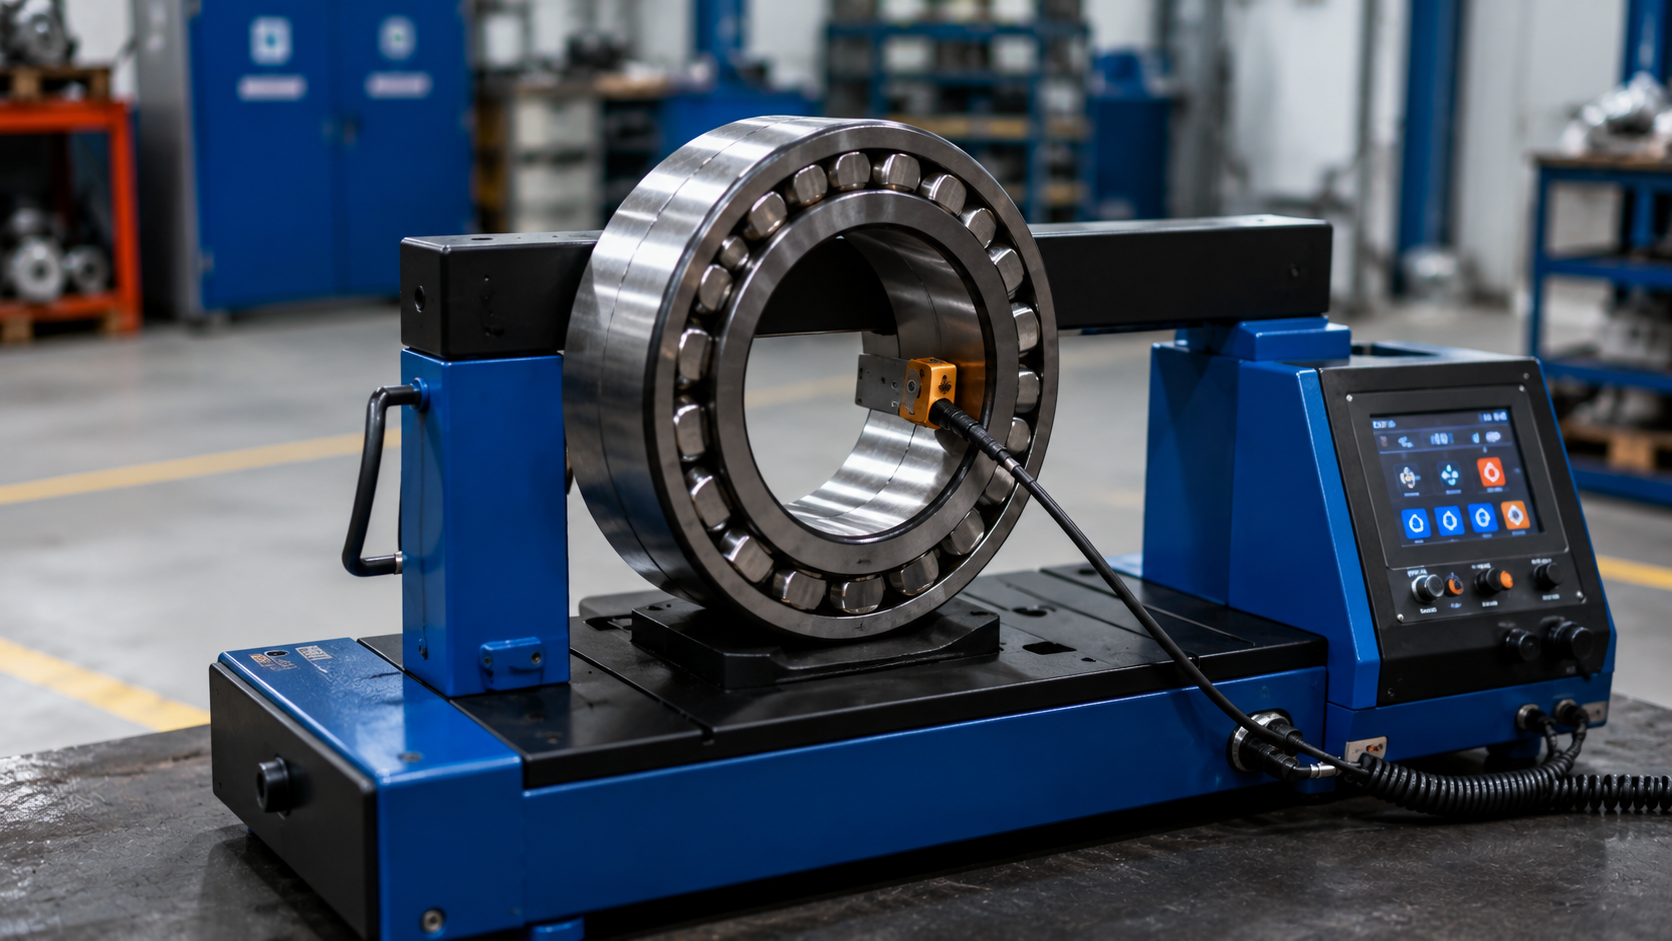
A bearing induction heater works by generating an alternating magnetic field around a coil and iron core, which induces eddy currents inside the bearing’s steel rings. Electrical resistance converts those currents into heat directly within the metal, expanding the inner ring so it slides onto the shaft without force. Heating is fast, contactless, oil-free and reversible in seconds.
| Operating principle | Faraday’s law — eddy current + hysteresis heating |
| Standard max bearing temperature | 110 °C (open bearings) — never exceed 120 °C |
| Sealed / greased bearings | Limit to ~80–100 °C (grease and seal material dictate) |
| Typical mounting ΔT | 80–90 °C above shaft temperature |
| Steel thermal expansion | ≈ 12 × 10⁻⁶ per °C (per mm of bore diameter) |
| Typical heating time | 2–15 minutes depending on bearing mass and unit kVA |
| Residual magnetism after cycle | < 2 A/cm with automatic demagnetisation |
| Energy efficiency vs oil bath | Substantially higher — heat is generated inside the part, not the medium |
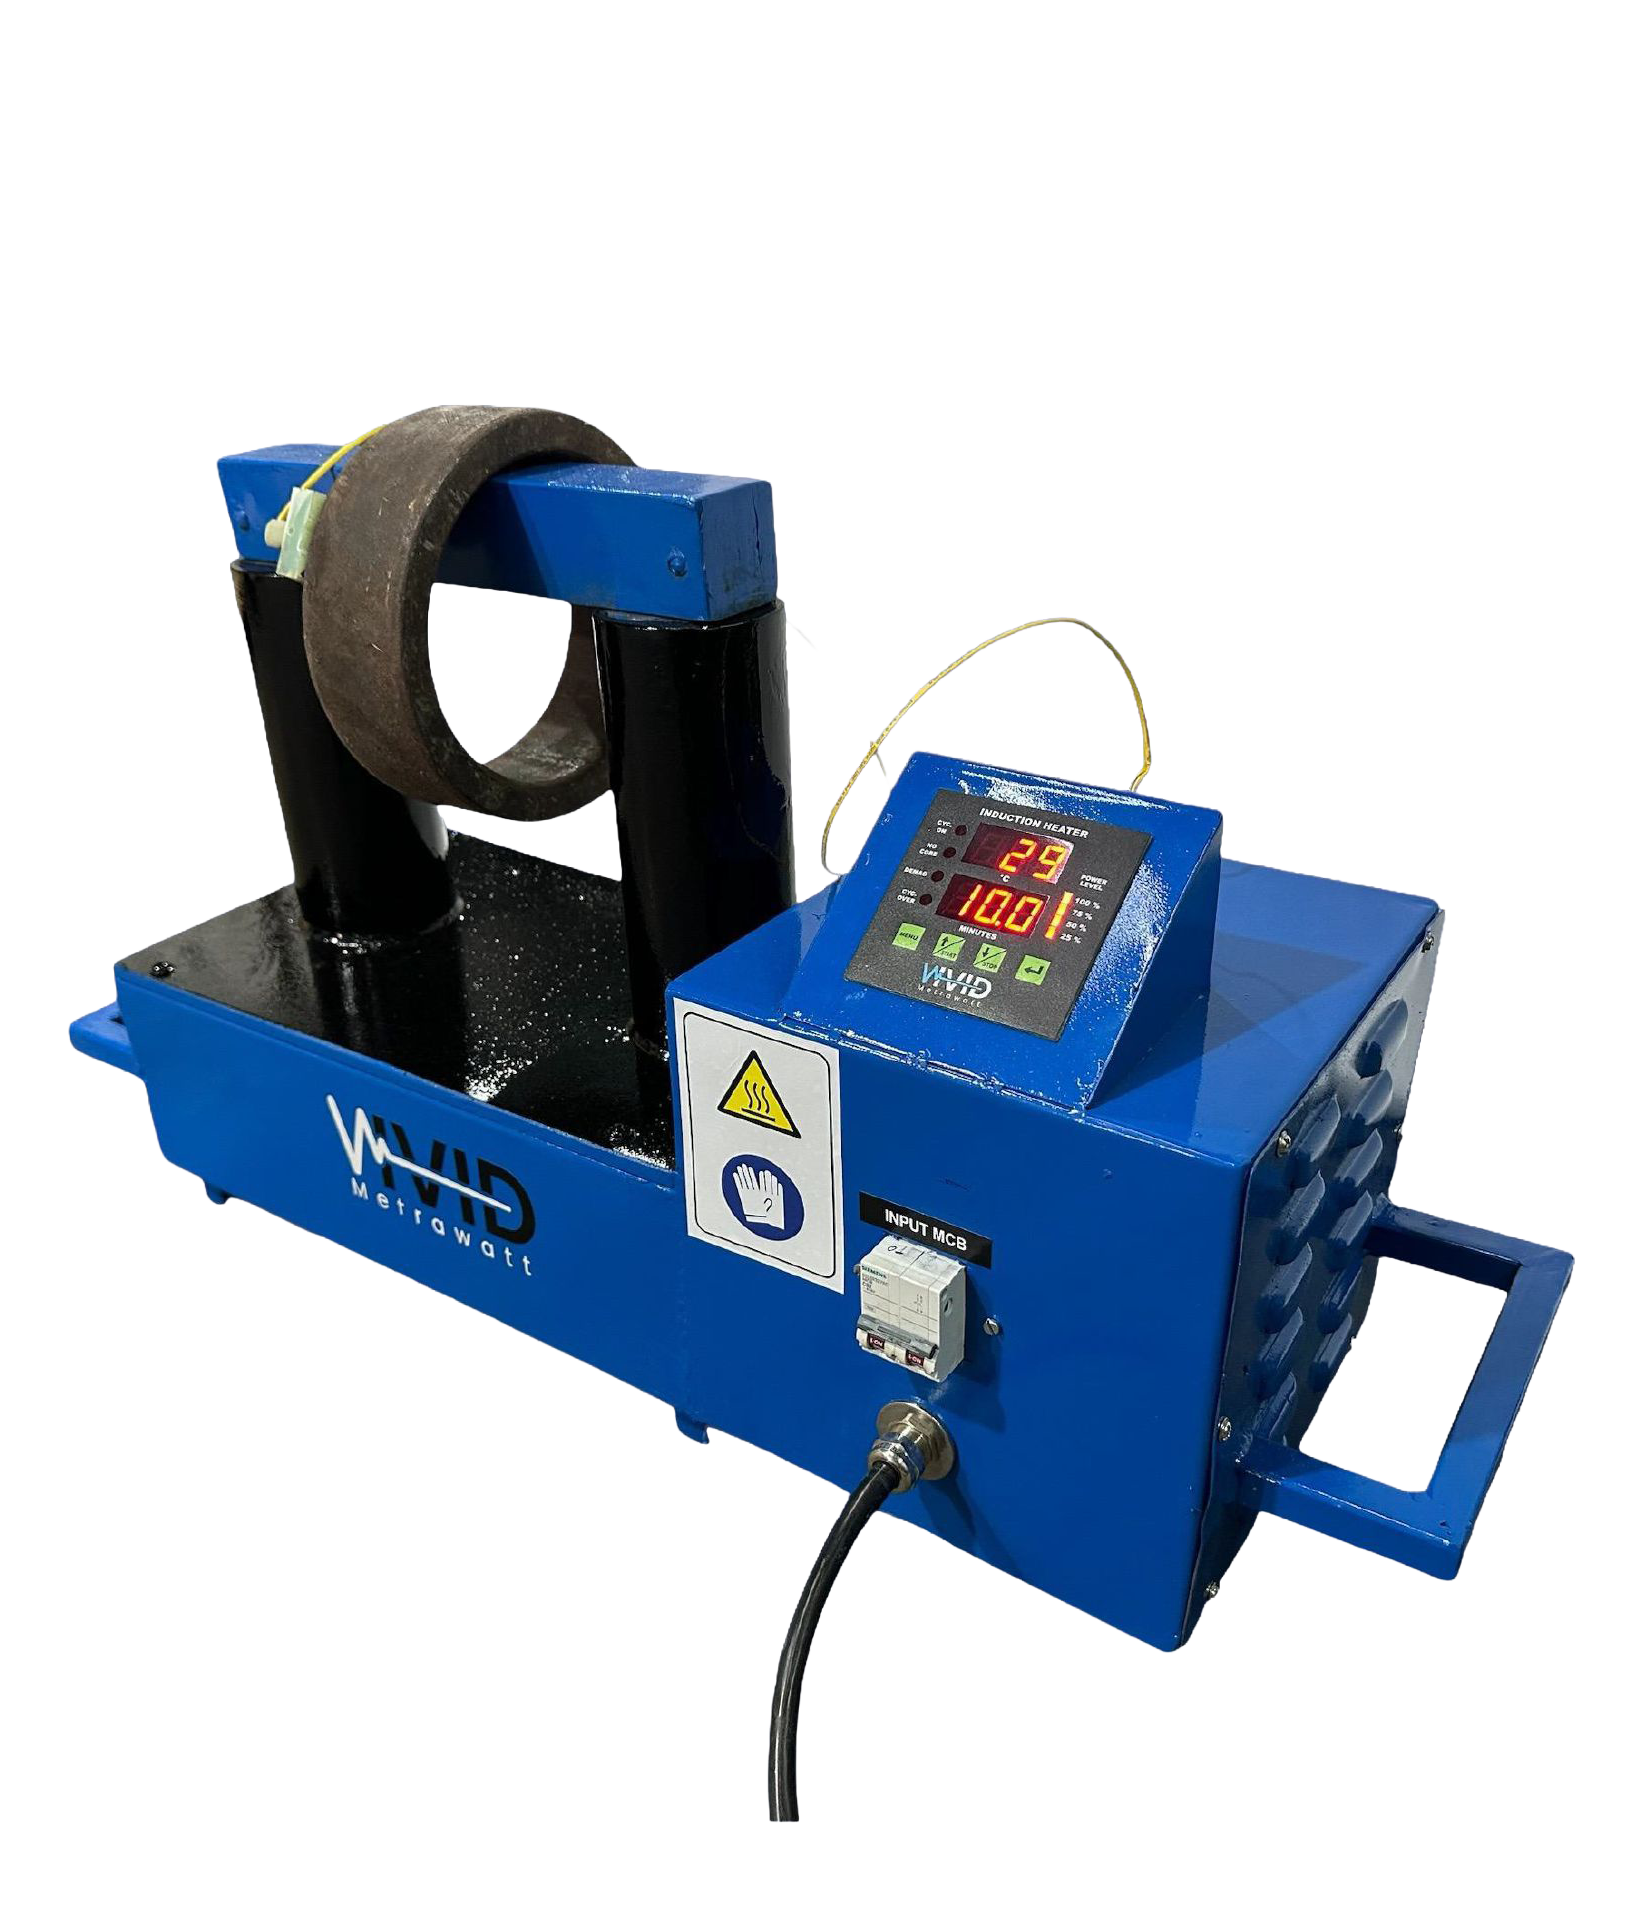
A bearing induction heater is an industrial tool that heats bearings and other ring-shaped ferrous components from the inside out, using electromagnetic induction rather than an external heat source.
The bearing itself becomes the secondary winding of a transformer. Current flows in the coil, magnetic flux passes through the laminated iron core and yoke, and the closed steel ring of the bearing carries induced current — which turns into heat through its own resistance.
Why this matters practically: the coil stays cool, no oil touches the bearing, no flame contacts the raceway, and heating stops the instant power is cut.
The sequence is:
This is the same physics described in our guide to how electromagnetic induction works — applied deliberately as a heating tool rather than a power-generation mechanism.
Two important behaviours:
This is the question most guides skip. Get it wrong and you destroy the bearing before it ever turns.
| Bearing type | Recommended max temperature | Reason |
|---|---|---|
| Open / non-sealed ball & roller bearings | 110 °C (absolute ceiling 120 °C) | Above ~120 °C, dimensional stability of standard hardened steel is compromised |
| Sealed bearings (2RS, 2RZ) | 80–100 °C | Seal elastomer degrades; grease may separate |
| Pre-greased / shielded bearings | 80–100 °C | Grease base oil bleeds and lubrication life drops |
| Bearings with polyamide cages | ~100 °C | Cage material limit is lower than the steel limit |
| Heat-stabilised bearings (S1, S2 suffix) | Per manufacturer datasheet | Specifically treated for elevated service |
Non-negotiable rule: never exceed 120 °C for a standard bearing. Exceeding it can reduce hardness, alter internal clearance permanently, and cause premature raceway failure — often weeks later, making the root cause hard to trace.
Always heat to the bearing’s target temperature, not the heater’s set point. Use the magnetic temperature probe placed on the inner ring, and set the controller to auto-stop on temperature, not on time.
The bore must expand more than the interference fit, with clearance to spare for handling time.
Formula:
ΔT = (I + C) / (α × d)
Where:
Worked example — 100 mm bore, 0.045 mm interference:
ΔT = (0.045 + 0.05) / (0.000012 × 100)
ΔT = 0.095 / 0.0012
ΔT ≈ 79 °C
With a shaft at 25 °C ambient, the bearing target is roughly 104 °C — comfortably under the 110 °C limit.
Practical shortcut: for most standard interference fits, ΔT of 80–90 °C above shaft temperature is correct. If your calculation demands more than 90 °C above ambient, re-check the shaft tolerance — the fit itself may be wrong.
After heating, the bearing retains residual magnetism from the applied field. If left magnetised, the bearing behaves like a magnet in service:
A proper bearing induction heater performs demagnetisation automatically at the end of each cycle by reversing and progressively decaying the field. Target residual magnetism is below 2 A/cm.
This is a genuine differentiator. Oil baths, hot plates and ovens do not magnetise the bearing at all — but they bring their own problems (contamination, uneven heating, fire risk). Induction gives you clean, fast, controlled heating and removes the magnetism it creates. A heater without automatic demagnetisation should be treated as incomplete.
| Component | Function | What to check |
|---|---|---|
| Laminated iron core | Carries magnetic flux with low loss | Lamination tightness; audible buzzing indicates loosening |
| Primary coil | Generates the alternating field | Insulation condition, no discolouration |
| Removable yoke | Closes the magnetic circuit through the bore | Correct size for the bore — the single biggest efficiency factor |
| Magnetic temperature probe | Measures actual bearing temperature | Calibration; must contact the inner ring |
| Controller | Temperature/time modes, demag cycle | Auto-stop function working |
| Support arms / cradle | Holds the bearing safely | No deformation, secure locking |
Yoke selection rule: always use the largest yoke that fits the bore. An undersized yoke leaves an air gap, drops efficiency sharply and lengthens heating time. Our range of bearing induction heaters ships with graded yoke sets for exactly this reason.
For dismounting rather than mounting, induction heating for bearing removal covers the outer-ring technique, and induction shrink fitting covers couplings, gears and larger interference assemblies.
| Induction heater | Oil bath | Hot plate | Open flame | |
|---|---|---|---|---|
| Heating uniformity | Excellent (inner ring first) | Good | Poor | Very poor |
| Temperature control | Precise, closed-loop | Approximate | Poor | None |
| Contamination risk | None | High (oil residue) | Low | High (soot, oxidation) |
| Speed (100 mm bearing) | Minutes | 20–40 min | 30+ min | Fast but uncontrolled |
| Fire / burn hazard | Low | High | Moderate | Very high |
| Sealed bearings | Safe within limits | Not recommended | Risky | Never |
| Demagnetisation | Automatic | Not required | Not required | Not required |
| Local overheating risk | Low | Low | High | Extreme |
| Recommended for production | Yes | Legacy only | No | No |
The verdict maintenance teams reach: flame heating destroys bearing metallurgy invisibly, oil baths contaminate and create fire risk, hot plates heat unevenly. Induction is the only method that combines speed, control and cleanliness.
| Symptom | Likely cause | Corrective action |
|---|---|---|
| Bearing heats very slowly | Undersized yoke / large air gap | Fit the largest yoke that passes the bore |
| Temperature reading erratic | Probe not seated on inner ring, or magnet contaminated | Clean and reposition probe on clean steel |
| Unit trips on overload | Supply voltage low, or bearing mass exceeds unit rating | Verify supply; step up to a higher-kVA model |
| Loud buzzing from core | Loose laminations or yoke not seated fully | Re-seat yoke; if buzzing persists, service the core |
| Bearing won’t slide on after heating | ΔT under-calculated, or too much delay before mounting | Recalculate ΔT; pre-stage tools before heating |
| Bearing sticks partway on the shaft | Cooling started mid-mount | Do not force. Remove, re-verify fit, reheat |
| Debris collecting on bearing in service | Demagnetisation cycle skipped or faulty | Run demag cycle; verify residual field < 2 A/cm |
| Controller unresponsive | Supply phase loss or control fuse | Check incoming phases and internal fuses |
Operator safety
Preventive maintenance
For a broader review of interlocks, thermal cutoffs and enclosure protection, see our guide to induction heater safety features. If you are still deciding on capacity, how to choose an induction heater walks through bore range, mass and duty-cycle sizing.
Heat the bearing to approximately 80–90 °C above the shaft temperature, and never exceed 110 °C for standard open bearings or 120 °C under any circumstance. Sealed and pre-greased bearings should be limited to 80–100 °C to protect the seal material and grease.
Typically 2–15 minutes, depending on bearing mass, bore size, yoke fit and the unit’s kVA rating. A 100 mm bore bearing on a correctly sized yoke usually reaches target in under 5 minutes.
Yes, but with a reduced temperature limit of roughly 80–100 °C. Always confirm the seal material and grease specification with the bearing manufacturer before heating.
Residual magnetism attracts ferrous wear particles into the lubricant film, causing raceway indentation and premature spalling. Quality induction heaters run an automatic demagnetisation cycle that reduces residual magnetism to below 2 A/cm.
For nearly all applications, yes. Induction heating is faster, contamination-free, precisely controlled and eliminates the fire hazard associated with heated oil. Oil baths remain in use largely as legacy equipment.
Above roughly 120 °C, standard bearing steel begins to lose hardness and dimensional stability. Internal clearance changes permanently, and the bearing typically fails weeks or months into service — long after the mounting error is forgotten.
Always the largest yoke that passes through the bearing bore. A larger yoke reduces the air gap in the magnetic circuit, which directly improves heating speed and energy efficiency.
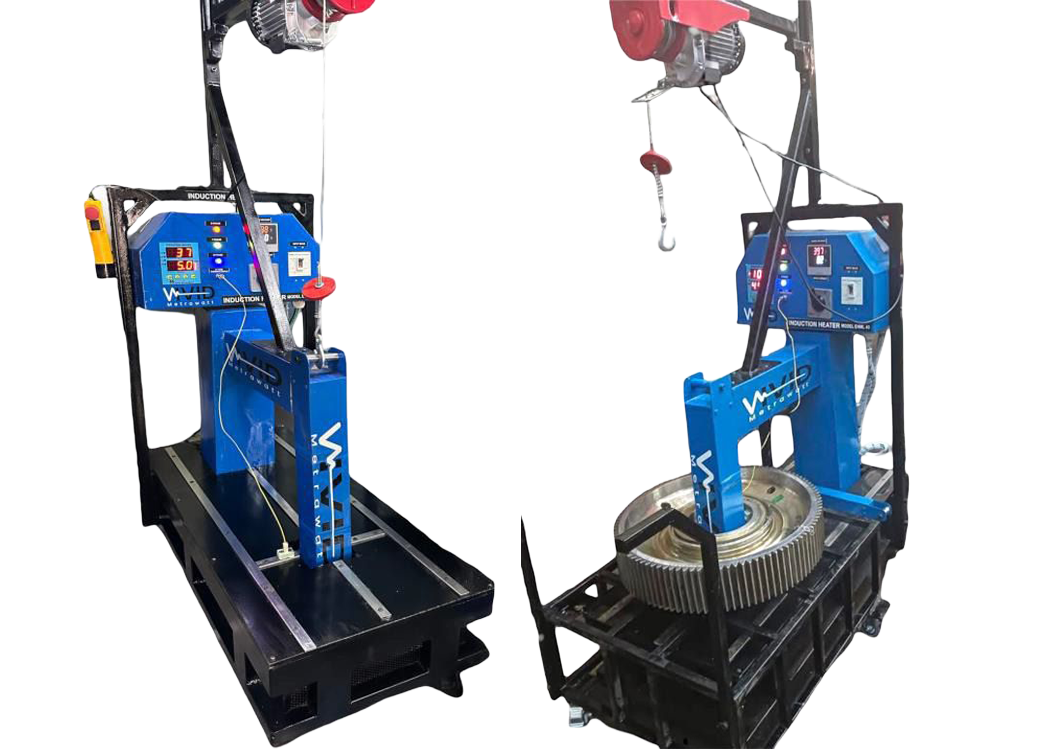
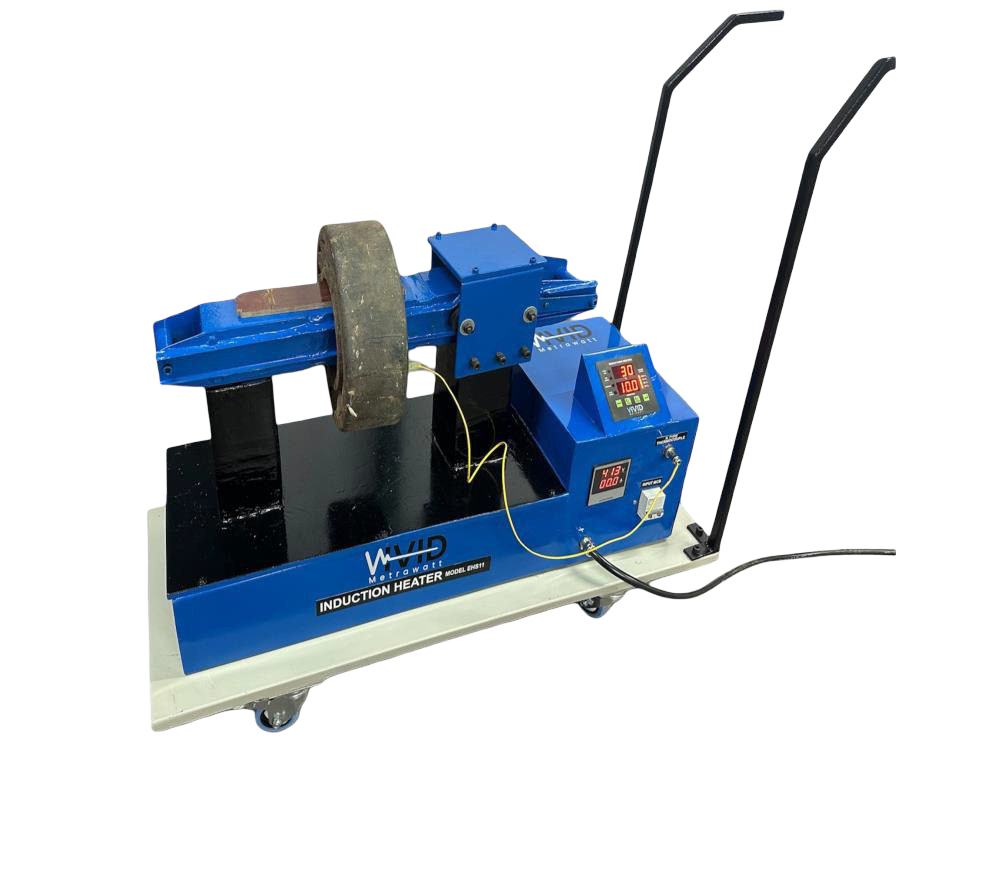
From compact EHML units for workshop maintenance to 44kW systems for heavy industry — our bearing induction heaters ship with graded yoke sets, calibrated probes and automatic demagnetisation as standard. Tell us your bore range and bearing weight, and our engineers will size the right unit.
Get a Sizing Recommendation View Bearing HeatersManufactured in Mumbai • Global supply • Operator training included